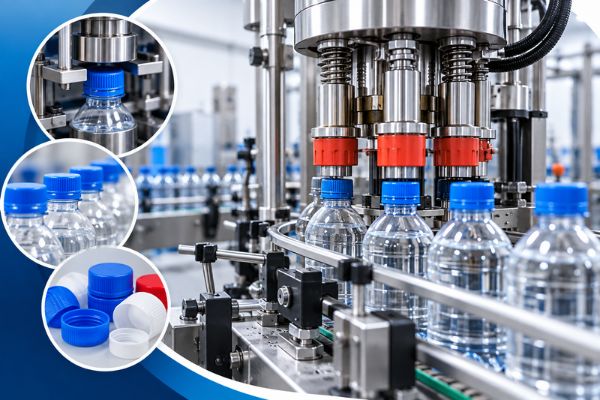
Why Closure Quality Should Come Before Capping Speed
A bottle can leave the filling station with the correct volume and still become a rejected pack. A crooked cap, damaged thread or poorly fitted closure can undo the work already completed. Choosing a Bottle Capping Machine Supplier means looking beyond bottles per minute to the quality of finished packs.
The strongest buying question is simple: can the proposed machine handle your bottle and cap combination consistently? A machine that performs well with one closure may need different tooling or adjustments for another.
For pharmaceutical, cosmetic and other liquid packaging lines, a useful supplier discussion starts with samples, closure requirements and production conditions. This guide explains how to turn those details into a better purchasing decision.
What Should a Bottle Capping Machine Supplier Evaluate First
A supplier should evaluate the complete package rather than recommend equipment from bottle volume alone.
Two bottles with the same capacity may have different neck finishes, heights or body shapes. Their caps may also differ in diameter, thread design, liner or tamper evident features.
Send production samples and drawings where available. Include every format you expect the machine to run.
| Packaging Detail | Why the Supplier Needs It |
|---|---|
| Bottle Material and Shape | Determines handling and gripping needs |
| Neck Finish | Helps confirm closure compatibility |
| Cap Design and Dimensions | Guides feeding and tooling selection |
| Liner or Sealing Insert | Affects the closure testing plan |
| Filled Product | Helps assess spills and cleaning needs |
| Required Output | Supports machine and line selection |
| Format Changes per Shift | Reveals changeover requirements |
Agree on the approved bottle and cap combinations before finalising the quotation.
Why Different Closures Need Different Capping Methods
Screw caps, roll on pilfer proof caps and press on closures do not use the same application method.
A screw cap is tightened onto an existing threaded neck. A roll on pilfer proof closure requires suitable rollers to form the aluminium cap around the bottle finish. A press on closure needs controlled downward force.
Even within one closure type, cap geometry can affect feeding and tooling.
Avoid assuming that one machine can process every cap after a simple adjustment. Ask the supplier to identify which formats share tooling and which require additional parts or another capping system.
This matters when adding a new product. Approve the proposed packaging combination with the machinery supplier before ordering large quantities of bottles and caps.
How Do You Set the Right Screw Cap Torque
Torque is the turning force used to apply or remove a screw cap. Too little application torque can leave a closure loose. Excessive torque can damage components or make the bottle difficult to open.
There is no single torque value suitable for every package. The target should reflect the bottle, cap, liner and packaging component recommendations.
Ask how the machine controls application torque and how operators check the resulting closure.
Removal torque is a separate measurement and should not automatically be treated as equal to the machine setting. Define the test method, timing and acceptable range with your packaging team.
A cap that feels tight by hand has not passed a complete closure assessment.
What Should a Capping Trial Actually Prove
A trial should demonstrate accepted output using representative production samples. A short run with selected bottles may not reveal feeding interruptions or variation between components.
Agree on the trial quantity and acceptance criteria beforehand. Include your regular formats and any combination likely to be difficult.
Check:
- Cap orientation and feeding consistency
- Correct seating without visible tilt
- Bottle stability during capping
- Thread, cap and tamper band condition
- Screw cap torque where applicable
- Closure performance under agreed tests
- Stoppages and operator intervention
Record good packs, rejected packs and stopped time. This gives a clearer picture than the displayed running speed.
For pharmaceutical applications, the trial should support your defined qualification and packaging requirements. A machine demonstration alone does not establish product shelf life or regulatory compliance.
Can Faster Changeovers Make a Bigger Difference Than More Heads
Adding capping heads may increase potential output, but frequent format changes can still consume production time.
A line running several bottle sizes needs practical adjustments and clearly identified change parts. Ask the supplier to demonstrate a complete changeover between your formats.
Time the process through to the first accepted bottle. Include feeder adjustments, guide settings, tooling changes and inspection.
Check whether operators need special tools and whether settings are easy to repeat. Request a format specific setup sheet.
Compare the machine against your production schedule. A high speed model may offer limited benefit when short batches require long setup periods.
How Should the Capper Fit Your Existing Packaging Line
The capper must work with the filler, conveyors and downstream equipment.
Share the current line layout, conveyor height, bottle spacing and expected incoming rate. Discuss how the system responds when bottles stop arriving or the downstream conveyor becomes blocked.
Ask which detection functions are included. Missing cap detection, cap position checks and automatic rejection may be available, but they should be confirmed in the quotation.
Capping and induction sealing are separate processes. If your pack requires an induction liner, confirm how the capper and sealing equipment will be coordinated.
Check performance across the connected line rather than testing each machine only in isolation.
What Support and Documentation Should You Request
Before ordering, request the operating manual, maintenance schedule, spare parts list and training scope.
For buyers in Ahmedabad, Gujarat or elsewhere in India, clarify who handles installation and how service visits are arranged. Confirm support for the cap feeder, capping heads and controls.
Ask for a written list of approved formats, supplied change parts and exclusions. Where your quality system requires qualification documents, agree on those deliverables before purchase.
When approaching Abhishek Pharma, provide bottle and cap samples, your required output and the existing line layout. Request a recommendation and trial based on those details.
Conclusion
A suitable bottle capping machine supplier should help you prove closure quality with your packaging components. Compare accepted packs, changeover time, line behaviour and support alongside the purchase price.
Start with samples and written acceptance criteria. Then confirm the final configuration, tooling and service scope before placing the order. This gives your production and purchasing teams a shared basis for the investment.
Frequently Asked Questions
Send bottles, caps, liners and drawings for every planned format. Provide enough samples for a meaningful trial. Include filled samples or a suitable test arrangement when product behaviour affects bottle handling.
Do not assume both are supported. These closures use different application methods. Ask whether the proposed machine supports interchangeable systems or whether separate equipment is required. Confirm the approved configuration in writing.
Base the choice on required output, staffing, batch sizes and line layout. Semi automatic equipment may suit lower volumes. Automatic equipment may suit continuous lines, provided feeding, handling and changeovers match your packaging formats.
Agree on package specific closure tests with your quality team and supplier. Check representative samples under defined conditions. Torque checks and visual inspection can support assessment, but neither alone proves leak resistance.
The capping method, output requirement, feeder, head configuration, tooling and inspection options affect price. Also confirm installation, training, freight and taxes. Compare quotations against the same approved packaging requirements.
Integration may be possible after checking conveyor dimensions, bottle transfer, operating rates and control requirements. Share a layout and machine details. Request a clear description of any modifications and who is responsible for them.
Confirm approved formats, trial results, supplied tooling, output conditions and acceptance criteria. Review delivery terms, installation, training, warranty exclusions and spare parts support. Include required documentation in the purchase scope.